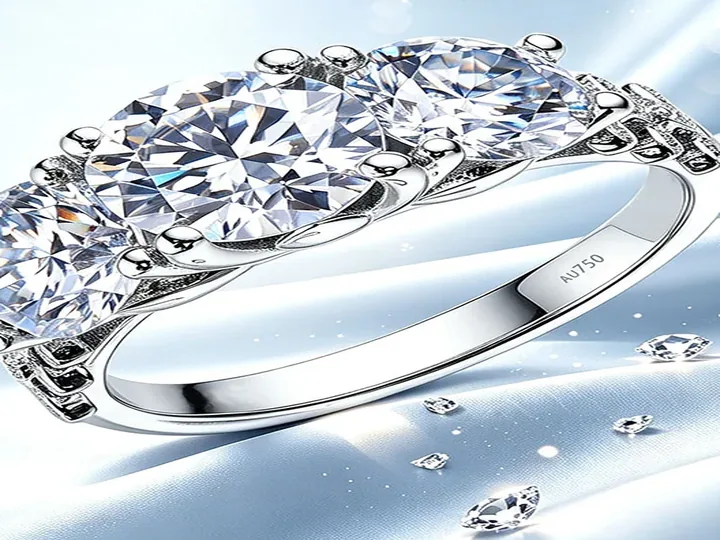
Cut for the finger, not the tray
A rough gemstone is cut twice in spirit: once for its optical return, and once for the metal it will live inside. Most buyers think only about the first decision - color, brilliance, fire - but the lapidary's choices around the girdle, pavilion, and culet determine whether a stone sets cleanly, sits level, and survives decades on a ring. A stone that photographs beautifully can still be a headache at the bench if it was cut for a collector's tray rather than a prong head.
The girdle is the line the metal grips
The girdle is the widest part of the stone, the edge where the crown meets the pavilion, and it is the line the prongs or bezel actually hold. A very thin, knife-edge girdle reads as elegant in a mounted view but is fragile: a prong can chip it during setting, and daily knocks can nick it over years. A very thick girdle solves the durability problem but adds dead weight - extra material the customer paid for, sitting hidden below the crown, and it pushes the stone visually higher in the head.
For prong settings, a medium to slightly thick girdle is the practical target. For bezels, the bench wants a consistent, predictable girdle thickness so the metal wall can burnish over it without cracking. When a factory requests calibrated stones for a production run, girdle thickness tolerance is part of the spec; variable girdles mean variable seating height, which means uneven stones across a run of identical rings.
Pavilion depth and the window problem
The pavilion is the lower, tapering half of the stone. Its depth controls how light behaves. A pavilion cut too deep pulls light out the bottom and the stone goes dark; a pavilion cut too shallow leaks light through the face and produces a washed-out look cutters call a window - you can see straight through the table to the background. Neither is strictly a setting fault, but both are reasons a stone bought loose disappoints once mounted, and a bench jeweler cannot repair an optical cut with a prong adjustment.
There is also a mechanical consequence. A very deep pavilion needs a taller seat and often a deeper basket, which changes the ring's profile against the finger. A shallow pavilion sits low and can rattle in a head sized for a normal stone. When a design calls for a specific head depth, the cutter needs that number before the stone is finished.
Culet, table, and orientation
The culet is the small facet or point at the bottom of the pavilion. A sharp point can dig into a seat and leave a visible pressure mark; a faceted culet distributes contact better. On stones set flush in pavé or channel, culet position relative to the band matters - a culet sitting proud of the seat can irritate the finger or catch on fabric.
Orientation is the under-discussed variable. Color zoning, silk inclusions, and pleochroism (different color from different angles) mean a cutter must decide which way the "good" direction faces when the ring is worn. Fine rubies and sapphires are almost always oriented to show their best face-up color, even at a small cost to brilliance. A stone cut for a pendant, viewed in motion from below, may be oriented wrong for a ring viewed face-up - another reason loose stones and finished jewelry are different products.
Calibrated stones versus hand-selected
Production settings are built around calibrated stones: fixed millimeter sizes that heads are manufactured to accept. A calibrated stone lets a factory stock heads and set from inventory. Fancy, hand-selected stones - a slightly off-round oval, a tapered emerald cut - demand custom-built heads or seat adjustment, which adds bench time per piece and kills interchangeability. For a retailer ordering a run of identical engagement rings, the cost difference between calibrated and hand-matched stones is real, and it shows up in both unit price and lead time.
Calibre cuts - small, precisely contoured stones set edge-to-edge in channels - are the extreme case: each stone is cut to fit a specific gap, so cutting and metalwork happen as a paired process, not a sequence. Side-stone mele face the same logic: matched color and size across a run matters more than the beauty of any single stone, because five slightly different mele around one center read as sloppy.
Polish and luster under the loupe
Finally, finish. A stone with poor facet polish - visible abrasion lines, dull junctions - scatters light and looks tired next to a well-polished equivalent, even at the same color grade. Bench jewelers also prefer crisp girdles that give a prong something to bite. A girdle that has been rounded and polished can let a prong slip sideways during setting. Ask to see stones under 10x before committing a run; the difference between production-grade and display-grade cut shows up immediately.
What to ask your stone supplier
When sourcing for a setting program, request more than color grade and clarity. Ask for girdle thickness, measured pavilion depth against the standard for that cut, culet type, and orientation notes. Confirm whether stones are calibrated to the head sizes you stock, and whether cut was prioritized for face-up appearance (right for rings) or weighted brilliance (often right for pendants and earrings viewed in motion). A supplier who answers these without hesitation is treating your job as a manufacturing partner, not a stone retailer.
Setting a stone is the moment all cutting decisions become visible. The cut that looked generous loose can sit too high, too deep, or too crooked once the prongs close - and by then the bench is repairing someone else's cutting choice rather than building your design. Discuss cut geometry with the lapidary before the stone is finalized, not after it arrives in the setting box. Compare our loose gemstones for calibrated inventory sized to production heads.
The International Gem Society moissanite guide explains how moissanite performs in daily wear compared with diamond.
Authoritative References
For buyers who need to verify the technical and regulatory basis of this guide, the following independent institutions publish authoritative reference data:
- GIA Gem Encyclopedia - independent grading and identification reference for natural and lab-grown gems.
- Wikipedia: Moissanite - peer-reviewed background on moissanite chemistry, optics and history.
Frequently Asked Questions
How do I verify a factory before placing a bulk order?
Request a production video, business license, export records and a paid sample run. A factory that accepts a 50-piece test order is usually a real manufacturer.
What payment terms do you offer?
30% T/T deposit with the balance against the bill of lading. This protects both sides on first orders and can move to net terms after a track record.
What is your normal reject rate?
3–5% under 10x loupe inspection for cast and set pieces. Defective units are replaced free in the next shipment.
Where is the factory located?
Wuzhou, Guangxi, China—the core lab-grown and moissanite manufacturing cluster. Shipments go via Guangzhou or Shenzhen ports.


